
The problem
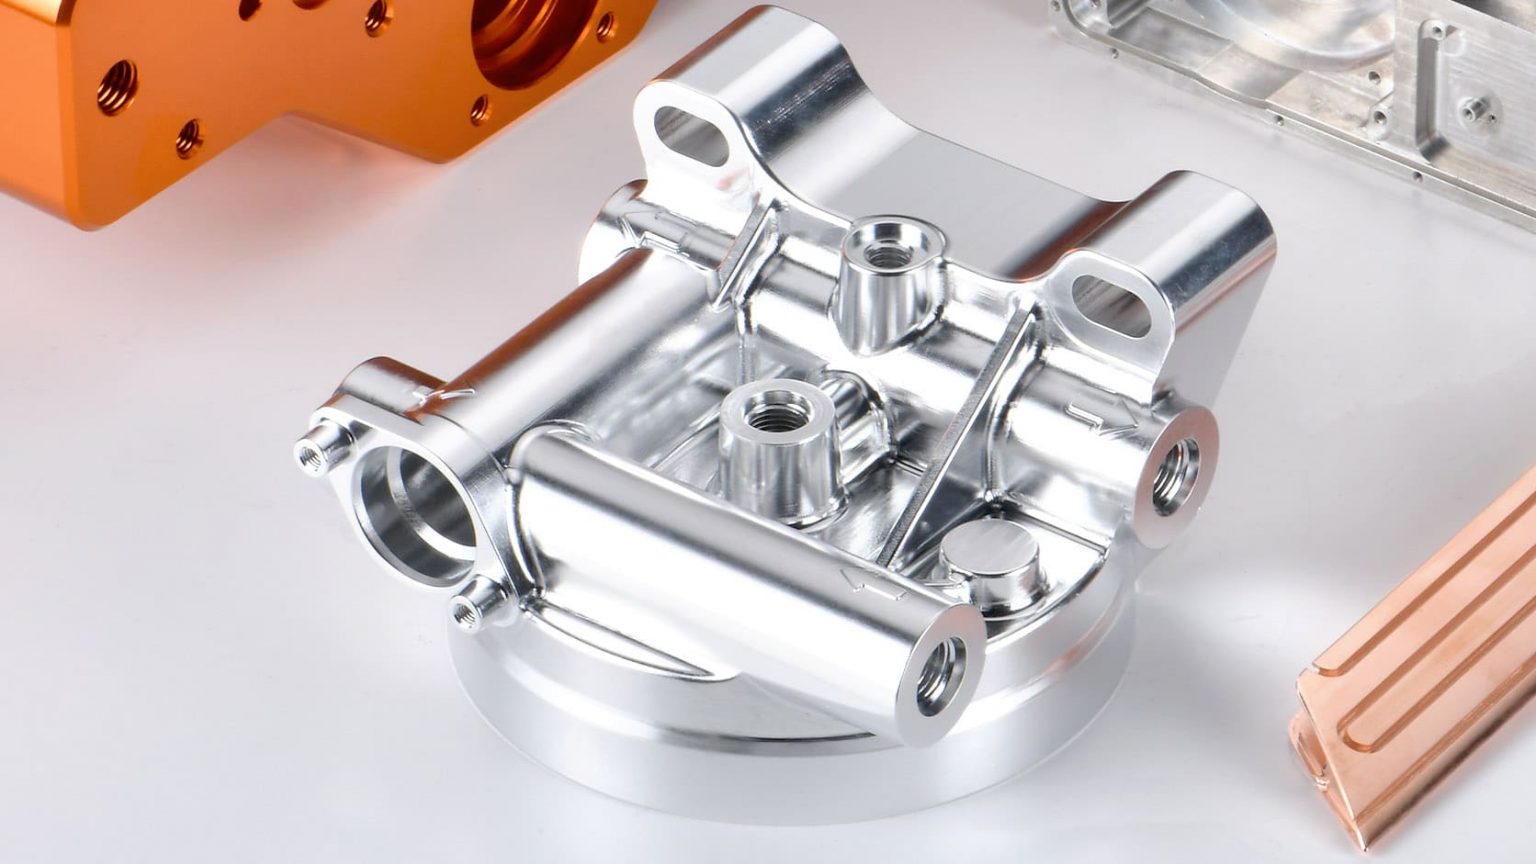
Prototypes that look good on screen but fail in reality are killing timelines and budgets. Teams rush design iterations, then discover tolerances, surface finishes, or fixturing needs weren’t accounted for. For hardware founders and engineering leads, a practical fix is reliable machining that handles complex geometry without endless manual rework — think robust 5 axis cnc machining services that get parts from CAD to verification faster.
Why five-axis matters
When features sit on compound angles or internal pockets, simple setups create stack-up errors. Five-axis cuts multiple faces in one setup, reducing cumulative tolerance error and avoiding extra fixtures. The trap is assuming every shop runs true five-axis procedures; the result is inconsistent surface integrity or expensive secondary ops. Tight geometry demands process discipline: fixture strategy, toolpath planning, and cutting parameters matter more than flashy machine specs.
Alternatives and trade-offs
Three-axis machining: cheaper and fine for prismatic parts, but expect added setups for angled features. Additive manufacturing: great for form and rapid iteration, but often needs finishing to meet fatigue and surface specs. EDM: perfect for delicate contours, yet slow and limited on certain alloys. The right choice pairs method to product intent — prototype for fit and form with fast methods, but validate functional metal parts with the process closest to production.
Experience, evidence, and a high-level anchor
I’ve led prototype programs that reduced iteration cycles by defining clear process gates: raw material traceability, first-article inspection, and controlled tool libraries. Industry practice shows aerospace hubs like Toulouse demand single-setup precision for complex airframe components — a requirement that validates why shops must master five-axis protocols. For teams sourcing production-alike hardware, look for suppliers experienced in handling the exact constraints of 5 axis cnc machining parts, with measurable inspection records and repeatable practices.
Common mistakes and how to avoid them
Skip these: accepting blanket lead times without process detail, assuming surface finish is automatic, and using generic fixtures for compound features. Do this instead: request fixture drawings, ask for sample toolpaths, require initial inspection reports, and verify cutting tool life for your alloy. Small upfront checks save weeks later.
Practical checklist for procurement
Define tolerances per feature, share true 3D models (not just drawings), specify material lot requirements, set inspection deliverables, and require a documented finishing plan for critical surfaces. Get agreement on metrics that matter: concentricity, hole positional tolerance, and surface roughness on functional faces.
Where this leads
Solve the specific manufacturing problem first: match the method to the function, insist on process transparency, and measure the outcomes. That approach naturally points you toward partners who consistently deliver production-like prototypes — the kind of partners aligned with Hanstar on quality and predictable results.